A laser-cut part can pass every dimensional check and still be rejected at goods-in because of a leaning face, a ribbed edge, or a dross bead the drawing never mentioned. ISO 9013 exists to stop that argument before it starts: it turns “a good cut edge” into two measurable numbers and a grade code that both sides of a purchase order read the same way.
Four facts frame what follows:
- The standard applies only when your drawing or delivery document references it; silence is the absence of a requirement, not a default grade.
- Two measurements carry the grade: u (how far the cut face leans from square) and Rz5 (profile roughness). Both limits scale with thickness.
- Laser cutting sits in scope from 0.5 mm to 32 mm. Above that, no grade code applies; you need an agreed sample instead.
- The grades cover geometry. Burr, dross, the heat-affected zone and part dimensions need their own clauses, or they will not be enforced.

What the Standard Covers, and What It Leaves to You
ISO 9013:2017, Thermal cutting — Classification of thermal cuts — Geometrical product specification and quality tolerances, is the current third edition, with a one-page Amendment 1 published in 2024. Its abstract states the scope: oxyfuel flame cuts from 3 mm to 300 mm, plasma cuts from 0.5 mm to 150 mm, and laser cuts from 0.5 mm to 32 mm. Buy 40 mm laser-cut plate and ISO 9013 does not classify that edge; a grade code on the drawing cannot make it apply.
The standard also states its own trigger condition: the specifications apply if reference is made in drawings or pertinent documents, e.g. delivery conditions. A supplier who delivers a rough edge on a drawing that never mentions ISO 9013 has not breached the standard, because the document was never invoked. The same document circulates as EN ISO 9013 (BS EN ISO 9013 in the UK).
TWI’s standards reference lists the factors the classification measures: perpendicularity and angularity tolerance, ten-point height of irregularities (the roughness family Rz5 belongs to), drag, and melting of the top edge. The last two are what an operator notices first when a cut looks wrong.
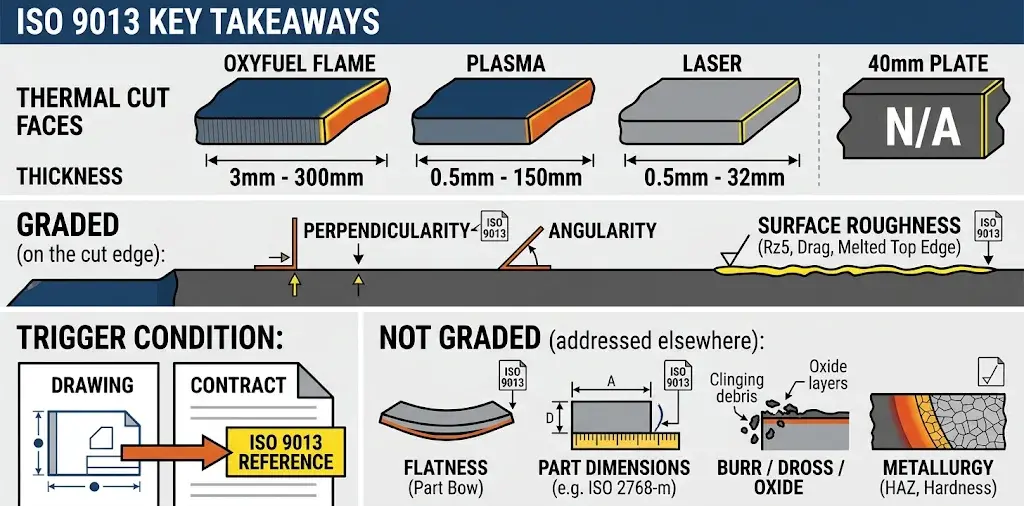
Just as important is what the standard deliberately leaves to other documents:
- Flatness. Not addressed; a part that bows after cutting is not an ISO 9013 nonconformity.
- Part dimensions. Handled by a general tolerance such as ISO 2768-m. A cut face can hit Grade 2 and still sit 0.4 mm off the nominal outline.
- Burr, dross and oxide. Not grading parameters; if clinging dross is unacceptable in your assembly, write it as a separate requirement with its own limit.
- Metallurgy. HAZ width, microhardness and corrosion resistance are heat effects; the grade describes the face, not what the heat did underneath it.
ISO 9013 supplies the vocabulary; the drawing decides what it means for your part.
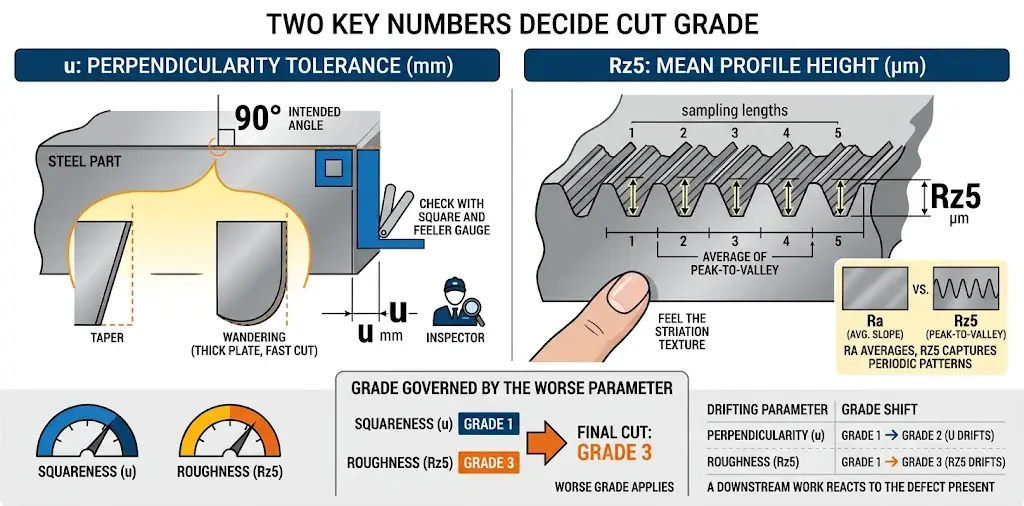
The cut grade is set by the worse of two metrics: u and Rz5
u, the perpendicularity or angularity tolerance, measured in millimetres, describes how far the cut face departs from its intended angle, normally 90° to the sheet. In practice u captures two defects at once: a face that leans consistently from top to bottom (taper), and a face square at the top that wanders at the bottom, produced by thick plate cut too fast. A lean is easy to check with a square and feeler gauge, so u is the parameter a receiving inspector can measure on the shop floor.
Rz5, the mean profile height, is measured in micrometres and averages the peak-to-valley height over five consecutive sampling lengths on the cut face. It is the depth of the striation texture you can feel with a fingernail. The standard uses a peak-to-valley parameter rather than Ra because a thermally cut face has periodic drag lines; an Ra average makes two visibly different edges read as similar.
Both limits must be met, and the worse of the two governs: an edge that hits Grade 1 squareness but Grade 3 roughness is a Grade 3 edge, because downstream work reacts to whichever defect is present. Which number moves when something drifts:
| What you see on the edge | Which number moves | Typical cause at the machine |
|---|---|---|
| Face leans consistently top to bottom | u worsens, Rz5 may stay good | Focus position, nozzle standoff, worn nozzle orifice |
| Square at the top, ragged at the bottom | u worsens sharply | Cutting too fast for the thickness, gas pressure too low |
| Fine, even striations | Both within grade | Nothing. Record the parameters as your baseline |
| Deep, widely spaced drag lines | Rz5 worsens first | Speed, focus, gas purity or pressure drift |
| Rounded, melted-over top corner | Top-edge melting (a named classification factor) | Excess power density at the surface, focus too high |
Tolerance limits rise with thickness, making roughness key
Limits rise with material thickness, because a thicker section holds more molten volume and takes longer to clear. The standard tabulates limits by thickness band; the trend behind those tables is captured by these expressions:
| Grade | Squareness limit u (mm) | Roughness limit Rz5 (µm) | Where it is normally seen |
|---|---|---|---|
| 1 | 0.05 + 0.003a | 10 + 0.6a | Thin sheet on nitrogen, sealing faces, tight fits |
| 2 | 0.15 + 0.007a | 40 + 0.8a | General precision laser work, ungrounded weld prep |
| 3 | 0.4 + 0.01a | 70 + 1.2a | Structural brackets, parts that get painted or coated |
| 4 | 0.8 + 0.02a | 110 + 1.8a | Non-critical profiles, edges that will be machined |
| 5 | 1.2 + 0.035a | not specified | Rough separation cuts, squareness only |

Put a thickness in and the numbers turn concrete:
| Thickness | Grade 1 (u / Rz5) | Grade 2 (u / Rz5) | Grade 3 (u / Rz5) | Grade 4 (u / Rz5) |
|---|---|---|---|---|
| 1 mm | 0.053 / 10.6 µm | 0.157 / 40.8 | 0.41 / 71.2 | 0.82 / 111.8 |
| 3 mm | 0.059 / 11.8 | 0.171 / 42.4 | 0.43 / 73.6 | 0.86 / 115.4 |
| 6 mm | 0.068 / 13.6 | 0.192 / 44.8 | 0.46 / 77.2 | 0.92 / 120.8 |
| 10 mm | 0.080 / 16 | 0.220 / 48 | 0.50 / 82 | 1.00 / 128 |
| 15 mm | 0.095 / 19 | 0.255 / 52 | 0.55 / 88 | 1.10 / 137 |
| 20 mm | 0.110 / 22 | 0.290 / 56 | 0.60 / 94 | 1.20 / 146 |
| 25 mm | 0.125 / 25 | 0.325 / 60 | 0.65 / 100 | 1.30 / 155 |
Computed from the expressions above to show magnitude; the standard lists limits by thickness band. For contractual acceptance, quote the standard’s table and edition year.
Two readings matter. On thin sheet the gap between neighbouring grades is about a tenth of a millimetre, so grade decisions there are effectively roughness decisions. On thick plate the roughness column does the damage: 155 µm at Grade 4 on 25 mm is a visibly ribbed edge no paint will hide.
Specify exact ISO 9013 grades on drawings to match each edge's function
A grade that is not written down is not a requirement. The most common failure mode in edge-quality disputes is a note reading “ISO 9013” with no grade code: the shop chooses, and shops choose the grade that runs fastest. The standard provides a designation string stacking the required classes (squareness, roughness, dimensional class) after the standard number; because templates label the segments differently, write the code and spell it out in words as well.
| Field | What to write | Why it matters on the floor |
|---|---|---|
| Standard and edition | ISO 9013:2017 + Amd 1:2024 | Stops a supplier quoting an older table |
| Grade code | Squareness class, roughness class, dimensional class | Turns "good edge" into a measurable limit |
| Thickness band | Every gauge on the part, per face | Limits change with thickness |
| Evaluated vs excluded zones | Which edges are graded, which are not | Pierce and cut-out zones are not representative |
| Measurement basis | Instrument, sampling position, number of readings, who measures | Two labs can disagree by 30% on the same edge |
| Burr / dross clause | A separate numeric or visual limit | ISO 9013 does not grade these |
| Retained sample | One signed first-article per grade per material | Converts future arguments into a comparison against a physical reference |
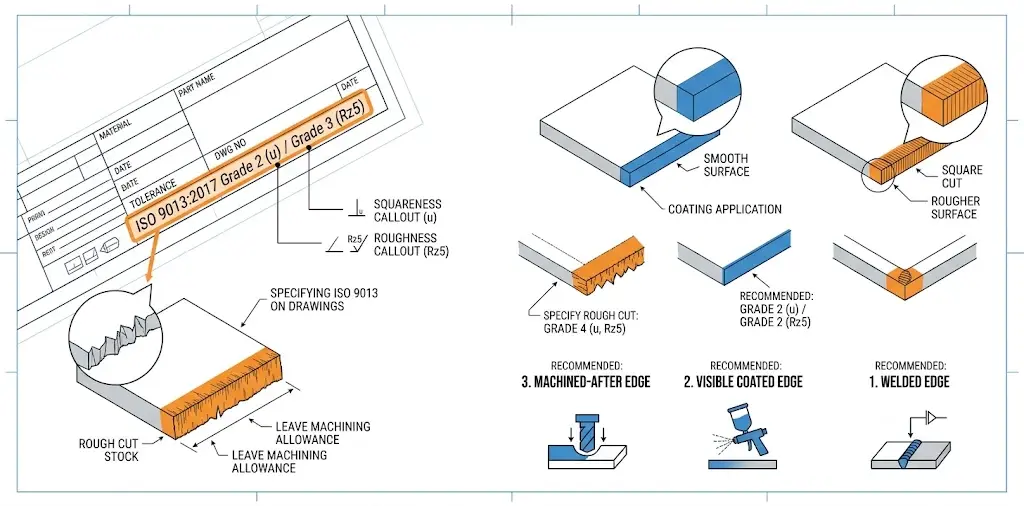
An illustrative note for a 10 mm Grade 2 sealing face:
Thermal-cut faces shall comply with ISO 9013:2017. Squareness and roughness classes: Grade 2 (u ≤ 0.22 mm, Rz5 ≤ 48 µm at 10 mm nominal thickness). Dimensional tolerances as dimensioned. Burrs and loose dross not permitted on assembly faces. Grade applies to continuous cut faces, evaluated at least 10 mm from pierce points.
Match the grade to the function of each edge, not to the strictest number on the sheet:
| Component application | Main quality priority |
|---|---|
| Electrical cabinet panels | Dimensional accuracy and consistent edges |
| Precision machine brackets | Perpendicularity and dimensional control |
| Welded structural frames | Joint fit-up and edge consistency |
| Decorative stainless panels | Surface appearance and edge finish |
| Heavy equipment components | Cut geometry plus machining allowance on finished edges |
A welded edge that the bead will consume needs squareness more than smoothness, so Grade 2 squareness with Grade 3 roughness is often the economical pair; a visible coated edge needs roughness control but tolerates more lean; machined-after edges only need to leave stock, which is Grade 4 territory at a lower price.
What Each Grade Costs, and Where It Pays Back
Tightening the grade costs money at the machine; loosening it costs money downstream. The mistake is looking at one side only:
| Grade | What the machine side pays | What the downstream side gets back |
|---|---|---|
| 1 | Slower feed, tight focus window, high-purity gas, fresh nozzle, frequent test cuts, shift-to-shift discipline | Welds or seals as-cut, no grinding, minimal deburr, stable coating appearance |
| 2 | Moderate speed penalty, controlled gas supply, monitored nozzle condition | Weld prep needs wire brushing at most; most cosmetic parts pass without rework |
| 3 | Near-production speed, standard gas, normal consumable life | Deburr and light dressing on visible edges; paint covers the texture |
| 4 | Full speed, minimal attention | Every functional or visible edge goes to a secondary operation |
The over-specification trap is grading a whole part Grade 1 because one edge is a sealing face; the rest of the perimeter pays for a grade it will never use. Grade the part edge by edge instead, and shops quote it cheaper. The reverse trap is silent under-specification: a Grade 4 edge with a clinging dross bead feeding a robotic weld fixture costs more in fit-up than the Grade 2 premium would have, and the cost lands in a different budget, which is why it never gets compared.
Exclude pierces, sharp corners, and tabs from ISO 9013 grading

A grade is an average statement about a face, and a laser does not deliver an average everywhere. Three zones read worse, each for a legitimate reason:
The pierce and lead-in zone. Penetration is drilling, not slicing, and the molten pool has nowhere to go. The face right after the pierce carries the roughest texture and worst squareness on the part, which is why the standard’s measurement practice avoids the start of the cut. If the drawing does not exclude a defined distance from the pierce, an inspector sampling there will fail edges that are acceptable everywhere else.
Sharp internal corners and small holes. At a sharp corner the machine decelerates and heat input per unit length rises, so the corner burns back. Below roughly one material thickness in diameter, hole quality degrades quickly as kerf and taper dominate the bore. Grading a 3 mm hole in 6 mm plate to the same class as the outer profile asks for a rejection no parameter change will fix.
Cut-out ends and tab locations. The last few millimetres of a cut lose gas flow support while the beam dwells; breakaway tabs leave a witness mark by design. Both belong in the excluded-zone note.
The fix is one sentence in the drawing notes, like the exclusion clause above; it does more for acceptance rates than any parameter change, because it stops the argument being about the wrong part of the edge.
Dross, Burr and HAZ: What the Grade Does Not Cover
The most common rejection reasons sit outside the grading system entirely; mixing them into a grade conversation turns a technical discussion into a commercial one:
| Condition | Does the grade capture it? | Where it belongs |
|---|---|---|
| Burr on the top or bottom edge | No | Separate clause with a height limit or a hand-deburrable note |
| Dross clinging to the underside | No | Separate clause: visual standard plus a signed sample |
| Oxide colour / heat tint on stainless | No | Cosmetic clause tied to welding, passivation or coating |
| HAZ width, hardness drop, sensitisation | No | Material or process specification, cross-section check if it matters |
| Face squareness and roughness | Yes, this is the grade | ISO 9013 code plus evaluation zones |
Dross in particular gets misread as a grade failure when it is usually a parameter or condition issue. The Fabricator’s guide to edge quality notes that oxidation build-up can come from low gas pressure or excessive speed, that exact nozzle centring is needed for the tightest tolerances, and that a contaminated lens or nozzle shifts the focus. None of those are grade problems; they are the difference between a machine that holds its grade and one that does not.
A bottom-edge burr also matters beyond cosmetics: on a later bend, a hard burr on the outside concentrates strain exactly where the outer fibre is already stretching. That belongs with the forming process rather than the cutting grade, covered in our guide to sheet metal bending.
Matching the Machine and Consumables to the Grade You Promised
A grade is a promise about consistency, not about a single good part. Any fiber laser produces one photogenic sample; holding Grade 2 across a shift, a material lot and a nozzle change is a machine-and-discipline question. Three things move the needle more than headline power:
Nozzle and lens condition. Everything the grade depends on passes through parts that wear. A slightly worn or off-centre nozzle moves Rz5 before any controller parameter does, which is why consumables belong on a scheduled interval rather than a change-it-when-it-looks-bad habit; nozzles and protective lenses are stocked line items in our spare parts and consumables programme.
Machine architecture matched to the production pattern. A single-table open machine suits job shops with frequent material changes. Where the grade has to hold across continuous production of the same thickness, the machine that stays thermally and mechanically stable between nests holds the grade more easily; that is the difference between our ULF open-type single-table machine and the ULE enclosed machine with automatic exchange table. The series is built to ±0.01 mm positioning and ±0.03 mm repeat positioning accuracy, which governs contour repeatability; that is not by itself an ISO 9013 guarantee, which only a cutting test on your material establishes.
Validation on your material. Grades do not transfer between materials at the same thickness: stainless on nitrogen, mild steel on oxygen and aluminium behave differently in both u and Rz5, and the limit does not care why. The only honest way to promise a grade is to cut your material, at your thickness, on the machine you are buying, and measure it.
These levers sit outside the standard but decide whether the grade holds:

| Lever | What it moves | Where we go deep |
|---|---|---|
| Assist gas type and pressure | Dross, oxidation, Rz5 stability | Assist gas: oxygen vs nitrogen vs air |
| Cutting speed | Drag lines, bottom-edge raggedness | Setting speed by material and thickness |
| Power, focus and nozzle setup | Taper, top-edge melting, kerf geometry | Cutting parameters explained |
| Kerf compensation | Part dimensions, hole size | Kerf width and compensation |
| Shared vocabulary | Reading the terms above consistently | Laser cutting terms glossary |
Final Thoughts
ISO 9013 rewards buyers who treat edge quality as a specification rather than an expectation. Write the grade code and edition on the drawing, name the excluded zones, agree the measurement basis, keep a signed first article, and most edge-quality disputes never start. If you are specifying a grade for the first time or upgrading a machine to hold one, send us your material, thickness and drawing requirement and we will cut a test blank, return it as a signed reference with the parameters it was run at, and help you compare configurations across the fiber laser cutting machine range.