For most shops: oxygen for carbon steel where an oxide edge is acceptable, nitrogen for stainless, aluminium and weld-ready or coated edges, compressed air for thin, non-cosmetic work with a properly engineered air supply. A starting point, not a specification.
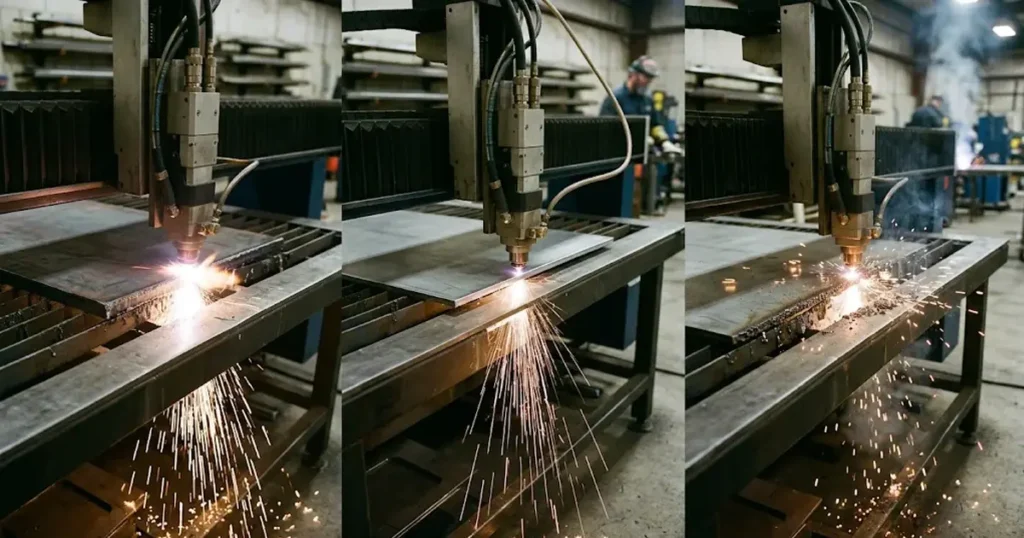
- All three eject molten metal from the kerf — the narrow slit the beam opens. Only oxygen adds energy.
- The edge is what your customer buys: welding, coating, bending and visible surfaces each set a different acceptance test.
- “Air is free” holds only until you specify dryness, oil and particles at the point of use — where gas reaches the cutting head.
- Gas type, purity, pressure, flow, focus and speed are one coupled setting; gas delivery belongs in the machine enquiry, not a later purchase order.
Compare cost per conforming metre, not cost per hour
Gas quotations arrive per cylinder, per cubic metre or per compressor hour. None decides the question: a fast cut that needs grinding and a slower cut that goes straight to welding are different products. Work in cost per conforming metre — one metre of edge your customer will accept:
C_m = (C_g + C_e + C_c + C_l) / (v × Y)
Build every term from your own records.
| Term | Where the number comes from | Usual mistake |
|---|---|---|
| C_g | Gas per laser-on hour: contract, rental, delivery, vaporiser losses; or compressor power, dryer, filters | Counting only purchase price; treating air as zero |
| C_e | Machine per laser-on hour, from your rate and throughput | A flat rate regardless of real throughput |
| C_c | Consumables per hour: nozzles, windows, ceramics, filters | Ignoring optics lost to contaminated air |
| C_l | Downstream labour: deburr, oxide removal, rework, inspection | Treating it as fixed when gas drives it |
| v | Qualified speed on your material, metres per hour | Copying a headline speed from another gas and criterion |
| Y | First-pass yield: accepted parts divided by parts started | Assuming 100%; colour and dross drift over a shift |
C_l and Y are outputs of the gas decision, not constants. Oxygen pushes cost out of C_g into C_l; air pushes it into C_c and Y; nitrogen raises C_g and often takes C_l near zero. The row most often filled in wrong is Y.
One rearrangement settles most arguments. If nitrogen adds ΔC_g per laser-on hour over oxygen, and the oxygen route needs t hours of cleaning per accepted part at labour rate w, nitrogen wins when ΔC_g < t × v × Y × w. Every term is yours to measure; published hourly figures are someone else’s material, nozzle and wage bill. Supply method belongs in C_g too — cylinders, bundles, bulk liquid or on-site generation for nitrogen; compressor, receiver, dryer and filtration for air. Compare the whole system, not the gas price.
Start from where the edge goes next
Write down the next operation for every part family. The first table answers the material question; the second is what supplier pages almost never provide. Read the right-hand column first — the downstream requirement decides the gas, not the material name.
| Material | Oxygen | Nitrogen | Compressed air | What decides it |
|---|---|---|---|---|
| Carbon steel | Common, thicker plate | Clean-edge option | Thin, non-cosmetic | Oxide tolerance, cleaning step |
| Stainless steel | Rarely for visible work | Usual choice | Only after a tint trial | Appearance, corrosion, weld prep |
| Aluminium | Process-dependent | Usual choice | Only after a tint trial | Reflectivity, finish requirement |
| Galvanised steel | Needs a trial | Often preferred | Needs a trial | Coating, fume handling, EHS sign-off |
| Copper and brass | Needs a trial | Commonly considered | Needs a trial | Machine-specific qualification |
| Where the edge goes | Oxygen | Nitrogen | Compressed air | Record in acceptance |
|---|---|---|---|---|
| Welded as-cut | Oxide must be removed | Usual default | Only if weld procedure is qualified on air-cut edges | Weld procedure, edge prep step |
| Powder coated or painted | Descaling usually extra | Clean face supports adhesion | Light oxidation; approved test panel | Adhesion test, colour, cleaning |
| Bent on a press brake | Deburr and remove oxide | Deburr still applies | Deburr plus edge check on thin stock | Burr height, bend distance, crack check |
| Visible stainless, food or medical | Discoloured face fails | Bright face required | Tint likely; test actual alloy and finish | Agreed sample under defined lighting |
| Blasted before finishing | Often lowest total cost | Pays for an edge blast removes | Viable if the edge spec allows | Whether blasting removes all oxide |
| Internal, unseen parts | Fine where oxide is tolerated | Usually unnecessary spend | Often the economic choice | Burr and dross limits only |
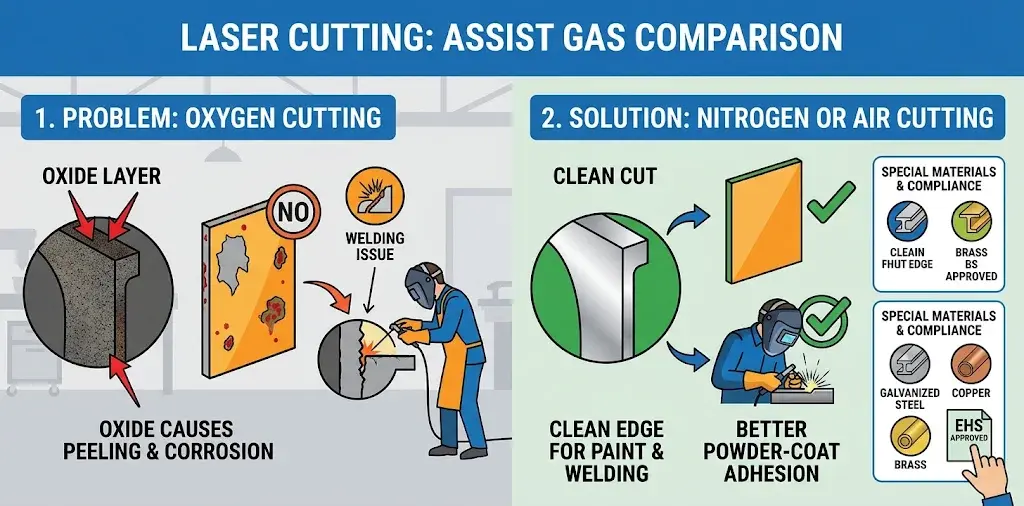
The 2015 FABRICATOR article states that “the oxide edge needs to be removed if the parts are headed for welding and (especially) painting.” Jeff Hahn, in Canadian Metalworking in 2011, adds the in-service failure: oxide left in place chips away and causes corrosion. A 2019 The FABRICATOR article on cut edges links oxide-free faces to better powder-coat adhesion and weldability — supplier-authored, so take the process logic, not its figures.
This is where “air is fine for painted parts” breaks down. Painted parts are viable on air only after the coating supplier approves a test panel and the criterion includes an adhesion test.
Galvanised stock and copper or brass need the same treatment: gas choice, fume extraction and site compliance are confirmed in writing by the equipment supplier and your EHS officer. Keep the matrix live — adding powder coating changes your gas economics without changing a cutting parameter.
Oxygen cuts thick steel fast, but requires post-cleaning and stability
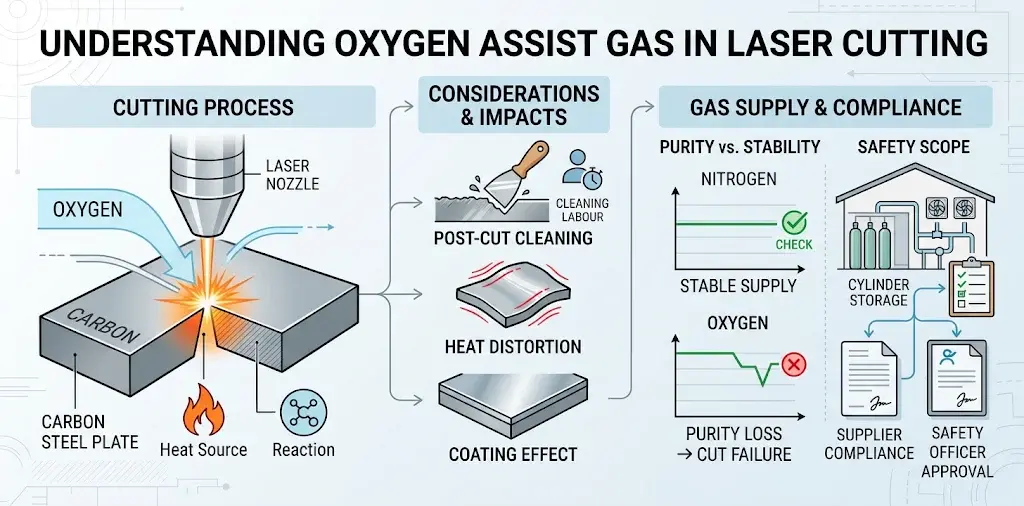
Oxygen is traditional for mild and carbon steel because the reaction supplies heat at the cut front — useful on thicker plate and lower-power machines. Flow is comparatively low, so the gas line is not the expensive part.
The invoice arrives later: cleaning labour before welding or coating (§3), higher heat input on distortion-sensitive parts, and a changed edge on coated stock. Purity behaves differently here. In the 2015 FABRICATOR overview, Mazak’s Mark Mercurio worries less about nitrogen’s absolute purity than about its stability, whereas a drop in oxygen purity sharply affects the ability to cut at all. Write stability into the supply specification rather than buying the cheapest oxygen.
Oxygen widens the safety scope: service cleanliness, cylinder or bulk storage, pressure-rated piping, relief and ventilation are specified before the system is ordered. We do not assert compliance — those come in writing from the supplier and your safety officer, against local regulations.
Nitrogen yields clean edges but demands stable supply and purity
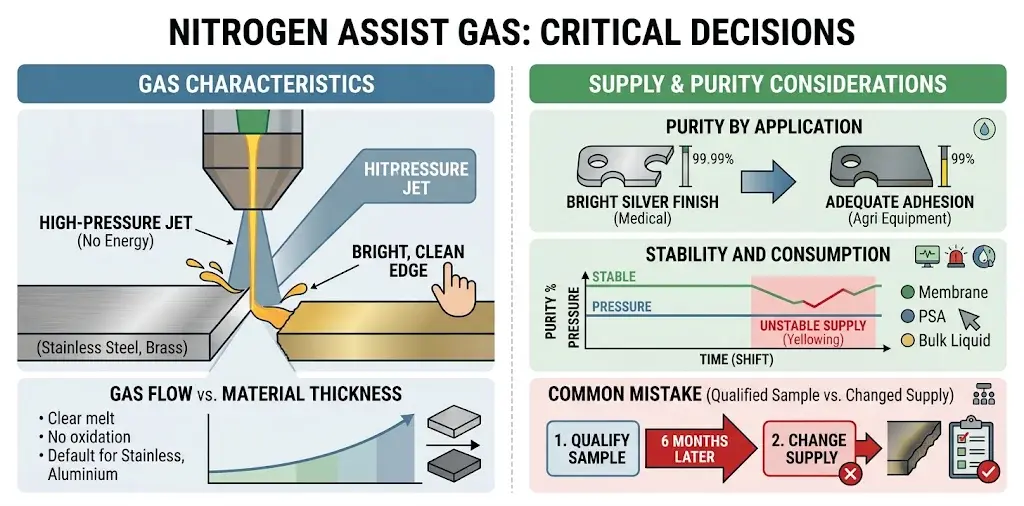
Nitrogen contributes no energy; a high-pressure, high-flow jet clears the melt, so the face stays bright. It is the default for stainless, aluminium, visible parts and edges going straight to welding or coating.
Purity is derived from the part, not maximised. A 2019 FABRICATOR article on the cut edge distinguishes a bright silver finish for medical work from adequate powder-coat adhesion on agricultural equipment: size the generator for the purity needed at peak flow, then verify it holds when several machines draw at once.
Stability matters as much as the nominal grade — a drifting supply shows up as yellowing across a shift, so ask about monitoring, alarm thresholds and refill behaviour. Consumption scales with the work: higher power and thicker material mean higher flow, and membrane, PSA and bulk liquid supply have different pressure, flow and purity envelopes. Choose from your own laser-on hours and peak simultaneous demand, not an advertised payback period.
The common mistake: qualify nitrogen on a sample, then change the supply six months later. Gas, generator sizing and edge criterion are one decision.
Compressed air offers economical thin-sheet cutting but requires strict filtration
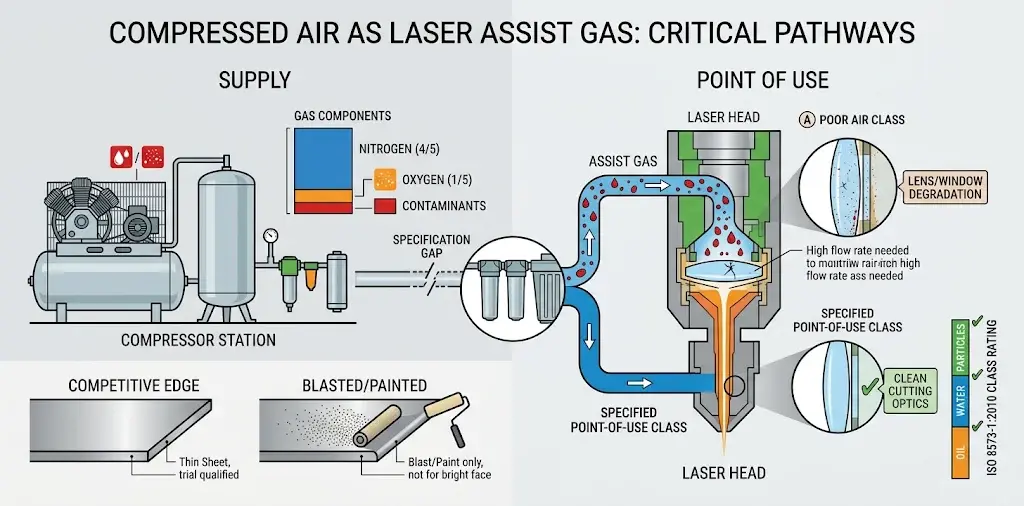
Air is roughly four-fifths nitrogen and one-fifth oxygen: some exothermic help, some oxidation on the face, and a cut often competitive on thin sheet. What the composition omits is everything the compressor adds.
ISO 8573-1:2010 specifies purity classes for particles, water and oil, “independent of the location in the compressed air system at which the air is specified or measured.” An air class is that rating. The key phrase is the last one: filters quoted at the compressor outlet and air reaching the head under full flow are not the same specification. Ask for the class at the point of use, the test method, and who re-verifies after filter changes. “We fit a dryer and filters” describes equipment, not a class.
Why it matters: moisture, oil and particulate reach the protective window. Hahn’s 2011 article describes damp shop air degrading the focal lens; the 2015 FABRICATOR overview adds that air cutting needs high pressure and flow, which plant compressors may not deliver cleanly. Budget a compressor sized for peak flow, receiver, dryer, staged filtration and monitoring into C_g and C_c of §2 — alongside laser nozzles, protective windows and other cutting consumables replaced more often when air is marginal, and gas-circuit maintenance intervals scheduled with the machine.
Air is cheapest where the edge will be blasted, painted under an approved test panel, hidden or structurally unimportant, on material qualified by trial. It is a poor shortcut when the drawing calls for a bright, as-cut face.
Three-way comparison: what changes when you switch
Use this table when a gas change is proposed; the last two rows are most often skipped.
| Decision dimension | Oxygen (O₂) | Nitrogen (N₂) | Compressed air |
|---|---|---|---|
| Role in the kerf | Exothermic reaction plus ejection | Inert high-pressure ejection | Partial reaction plus ejection |
| Supply infrastructure | Cylinders or bulk, oxygen-rated circuit | Bulk liquid, microbulk, cylinders, on-site generation | Compressor, receiver, dryer, staged filtration |
| Cost easy to miss | Cleaning labour and rework | Gas volume, tank rental, generator sizing | Optics, filter upkeep, yield drift |
| First check when quality drifts | Purity and pressure stability | Purity during refill and peak draw | Dew point, oil carryover, nozzle pressure |
| Re-qualification after switching | Full parameter set | Full parameter set | Full parameter set plus air class verification |
Two rows deserve emphasis. An oxide-free nitrogen edge can still carry dross or a hard burr — cleanliness is not the same as a burr-free edge. And every column in the bottom row requires a fresh focus, pressure, nozzle and speed qualification on the actual material — why gas changes fail in production.
Verify it on your own parts
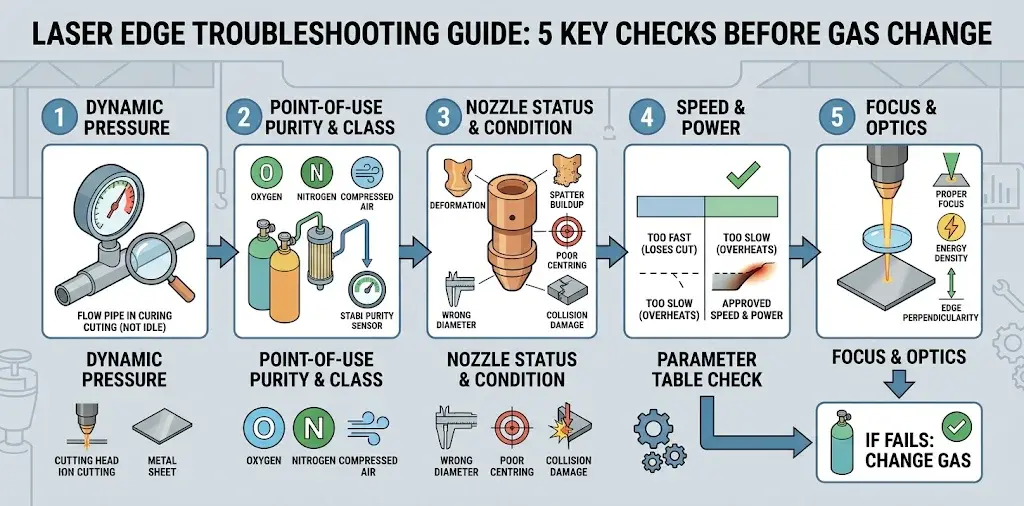
Before you blame the gas, fix these five
Burrs, rough edges and drift usually come from the coupled setting, not the gas type. Check in this order:
- Dynamic pressure at the head, measured during cutting — not the idle gauge reading.
- Purity or air class at the point of use, including behaviour during a refill or peak draw.
- Nozzle condition: deformation, spatter, wrong diameter, poor centring, collision damage.
- Speed and power against the approved parameter table; too fast loses the cut, too slow overheats the edge.
- Focus position and optics condition, which set energy density and edge perpendicularity.
If all five are stable and the edge still fails, change the gas.
A trial that settles it
A supplier’s sample was cut on their stock, nozzle, gas and criteria. Take adjacent coupons from one sheet — same heat, thickness, rolling direction and surface — and cut an identical set with each gas: a long straight edge, small hole, sharp corner and narrow web, where gas differences appear first.
Give each gas its own qualified focus, nozzle, pressure and speed; do not hold the nitrogen program fixed. Run enough parts to cover a shift, then send all three sets downstream and count accepted parts, not cut parts.
Record these fields for every gas; the final two feed C_m in §2.
| Field | Why it is needed |
|---|---|
| Grade, heat number, thickness, surface condition | Removes stock as a variable |
| Gas, nominal purity, supply method; air class measured at point of use | Ties edge colour to the supply and verifies it under flow |
| Nozzle type, diameter, condition, standoff | Flow is set at the nozzle, not at the tank |
| Head pressure, focal position, cutting speed | Makes the result reproducible |
| Piercing method and pierce time per part | Piercing can dominate thin-sheet economics |
| Laser-on time and parts per hour | Feeds v |
| Dross, burr, striation, colour against a written criterion | Turns "looks fine" into a record; specify ISO 9013 quality classes |
| Downstream steps and minutes per accepted part | Feeds C_l |
| Accepted parts divided by parts started | Feeds Y |
Agree the edge criterion with your customer first: a part that passes visual inspection and fails coating adhesion at the customer is not a conforming metre. We claim no gas is universally faster, cleaner or cheaper on your mix. If a parameter set needs diagnosis, remote diagnostics and parameter tuning for cutting heads and optics is one support function available to machine owners.
Specify the gas system in the same enquiry as the machine
The gas decision is usually made twice: once by the process engineer, and again, badly, when someone discovers the installed compressor cannot hold nozzle pressure at full flow. Fill the left column; make every supplier complete the right in writing. The row most often left blank is the air class at point of use.
| You supply | Supplier confirms in writing |
|---|---|
| Material grades, coatings, thickness range | Gas types qualified per material and thickness band |
| Monthly laser-on hours, peak concurrent machines | Nozzle pressure and flow at the head, not at source |
| Part families, batch sizes, edge destinations | Pressure-rated circuit, regulation and valve arrangement |
| Required edge criterion and downstream route | Nozzle library, protective window, consumable list |
| Whether compressed air will be used | Air class at point of use, test method, filtration train, re-verification after service |
| Whether nitrogen will be generated on site | Purity at peak flow, behaviour during refill, generator or bulk interface |
| Site constraints: power, floor, ventilation, storage | Storage options; what the quotation excludes |
| Acceptance and trial requirements | Trial-cut protocol, sample retention, written edge criterion |
| Operator and maintenance capability | Training scope: gas type, pressure, oxygen/nitrogen handling |
Before sign-off, ask for the specification sheet of the exact model and revision quoted: the gas circuit is part of the machine configuration. The CAMT fiber laser cutting machine range covers open-type, enclosed exchange-table and tube-cutting architectures, with different gas demand and duty cycles. An open-type single-table machine for smaller workshops and an enclosed exchange-table machine on batch work do not impose the same air-treatment load.
Second, name the people who will run it. operator training covering assist gas type and pressure, nozzle centring and oxygen/nitrogen handling is a separate line item, as is the wider service scope keeping the gas circuit, optics and consumables in specification after commissioning.
Send the worksheet with your material list, main grades, maximum thickness and monthly laser-on hours; ask for a written configuration and a trial cut on your own stock: contact the CAMT engineering team. We publish no universal gas price, cutting speed or purity figure, and do not assert compliance — those are established on your parts and signed off by the supplier and your site.