The middle of a part bends to a different angle because the ram and the table flex under load, so the punch does not go as deep at mid-length as it does next to the uprights. In air bending, punch depth sets the angle, so the middle comes out more open than the ends. That is the most common cause, but not the only one: tooling, material, program data and setup errors all produce the same complaint with a different signature. The sections below show how to read the signature, confirm the cause and fix it in the right order.
- Middle open, ends correct is the deflection pattern. The correction is crowning, not more ram depth.
- Middle tight or over-bent means the crowning value is too high for this job.
- One end open, the other closed is a taper, not a crowning problem. Check ram parallelism and table level.
- One spot off while the rest is right points at tooling: a die joint, a proud segment, local wear.
- Every station off by the same amount is program data, V opening or material grade, not a distribution problem.
- Measure at five stations before you change a setting. The profile tells you which cause you have.
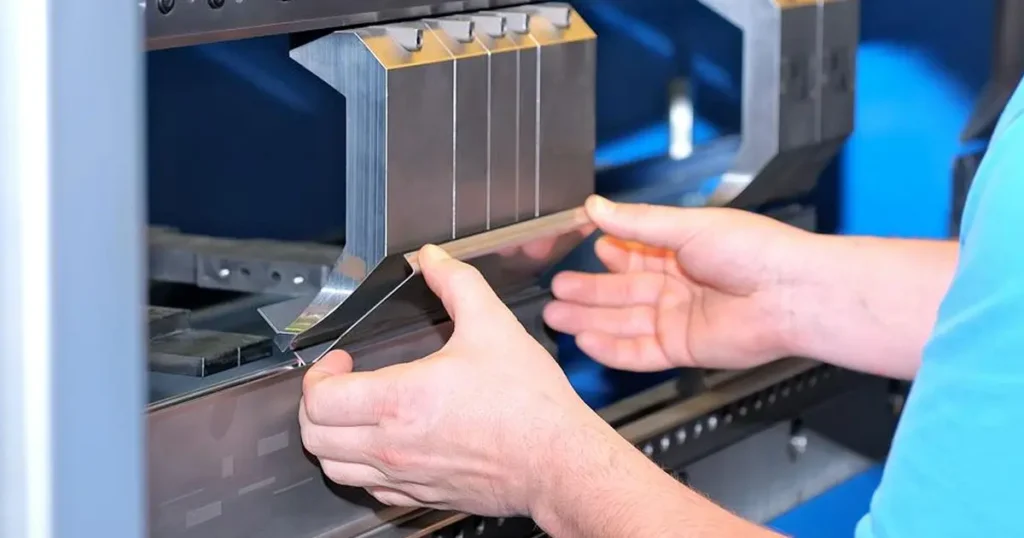
Why the Middle of the Part Bends Differently
A press brake loads its beams at the ends. The cylinders push on the ram close to the uprights, and the frame carries the table at the same two positions. Between them the ram bows upward and the table bows downward, so the gap between punch and die opens toward the center. The trade calls the resulting variation along the bend the canoe effect. The technical literature calls the same geometry the boat belly effect, and puts it in one sentence: angular precision depends on keeping punch penetration constant along the bending line, as this study of press brake frame deflection concludes.
Three points follow from that.
- It is normal. Every loaded press brake deflects. It is not evidence of a faulty machine, and it is the reason crowning systems exist.
- The ends are right for a reason. They sit next to the load points, where the beams deflect least, so a check taken at one end can pass while the middle is out. Always measure the middle.
- Describe the part by its profile, not its name. Writers disagree about which end of a canoe is on target. Five measured angles do not.
It also means no press brake is uniformly accurate at every length and load. The same structural study concluded that it is not possible to design a machine that produces uniform bend angles for every bending length, because the beam shapes that give parallel deflection at one span do not give it at another. The practical question is therefore not whether a machine deflects, but whether it carries enough compensation range for your longest and heaviest work, and whether the setup uses it.
How small movements become degrees
A published worked example fixes the scale: on 1 mm sheet in a 10 mm V die, a change of 0.05 mm in punch penetration changes the bend angle by about 1°, in the same study.
Set that against the machine. A modern servo-hydraulic control positions the ram to about 0.01 mm at each end, measured under the left and right pistons, as this guide to crowning on the press brake reports. The movement that spoils a bend is larger than that, and still invisible to anyone watching the stroke. On the same conditions, a 2° error in the middle is roughly 0.1 mm of penetration lost between the ends and the center, spread over meters of steel.
Two consequences run through the rest of this article.
- Depth per degree changes with the die. Penetration and angle are linked through the geometry of the V opening, so a wide die needs more ram travel per degree than a narrow one, and a sharp included angle is more sensitive than an open one. A crowning value that worked for 3 mm sheet in a 16 mm V does nothing useful for 1 mm sheet in an 8 mm V. Store settings per job.
- Narrow dies make everything worse. For the same thickness, a smaller opening gives more angular variation and is harder to compensate, as this analysis of angular variation explains. For air bending mild steel we use a V opening of six to eight times material thickness: six for tight radii, eight for thick or high-strength sheet, wider again for plate. Below six, expect more variation along the length and from bend to bend.
Step One: Measure Along the Bend, Not at One Point
The diagnosis lives in the profile, and a profile needs more than one reading. Six rules keep the data honest.
- Measure after the part is released. Read the angle with the ram retracted and the part off the die. A reading taken under load is not the angle you will ship.
- Pick one angle convention and write it down. Inside and outside angle give different numbers for the same part, and many arguments about a “wrong” part are two people reading different sides.
- Use five stations at minimum. Left end, quarter point, center, three-quarter point, right end. On parts longer than 2 m, read every 300 mm.
- Keep the gauge on the flat flange. On the curved bend zone it reads the tangent at that point, not the flange angle.
- Record the readings in order and note the orientation. Mark which end of the part was at the operator’s left. A profile without orientation cannot be compared with the machine.
- Repeat on a second part from the same setup. If the profile is the same both times, you have a geometry problem. If it moves, you have process drift.
The result is more useful than any single reading. A profile of 90.0° / 91.5° / 92.0° / 91.6° / 90.1° is a symmetric curve. A profile of 90.1° / 91.0° / 92.0° / 93.1° / 94.0° is a straight taper. A profile of 90.0° / 90.1° / 92.2° / 90.0° / 90.1° is a local defect. Three causes, three fixes, one measurement routine.
Six Patterns and Their Causes
Once the five-point profile is on paper, the rest is pattern matching. Each row gives the signature, the usual cause and a check that takes minutes at the machine.
| Profile pattern | What you see | Most likely cause | Five-minute check |
|---|---|---|---|
| Symmetric canoe | Ends on target, center open, smooth curve, worst at mid-length | Ram and table deflection under load; crowning too low or not fitted | Bend a short coupon at mid-bed. On angle while the long part is open in the middle means deflection |
| Inverse canoe | Ends on target, center closed or over-bent | Crowning value too high for this material, thickness and length | Set crowning to zero and bend one part. If the profile flattens or reverses, the compensation was overshooting |
| Linear taper | One end open, the other closed, roughly even progression | Unequal ram position (Y1/Y2), table twist, machine not level, backgauge not square, or a wedge-thick blank | Turn the part end for end and bend again. Error on the same side of the machine means machine or tooling; error that follows the part means material |
| Local step or dip | Four stations good, one spot off by 1° to 2° | Die block joint, proud punch segment, swarf or burr under a segment, local shoulder wear | Shift the whole tooling setup 200 mm to 300 mm along the bed and re-bend. If the defect moves with the tooling, it is the tooling |
| Uniform offset | All five stations off by the same amount | Program data, wrong V opening, springback allowance, wrong grade in the control, or tool height and seating after a tool change | Compare measured thickness and tooling against the program, not against the drawing |
| Not repeatable | Profile changes from part to part with no fixed shape | Thermal or hydraulic drift during the run, or material variation between sheets | Re-measure the same part twice, then bend two parts from the same sheet. Changing readings mean the process moved |
Two of these get blamed on the machine most often and are the cheapest to clear: the inverse canoe, which compensation itself created, and the local step, which belongs to the tooling.
Cause 1: Machine Deflection
Deflection depends on load, so it is predictable once you know what drives the load. Four factors set how much the middle loses.
- Bend length. The longer the bend, the more of the part sits under the deflected section of the beams.
- Tonnage per meter. Thickness, tensile strength and V opening all feed into it. High-tensile sheet needs more force, so it needs more compensation.
- Distance between the uprights. A longer unsupported span deflects more for the same load, and higher tonnage raises the need for compensation.
- Where the bend sits on the bed. Bending at mid-bed puts the work over the weakest section. Bending close to an upright puts it over the stiffest.
The coupon test
The cleanest test uses that last point. Bend a coupon about 300 mm long from the same material, with the same tooling and the same program, at mid-bed, and measure it. If the coupon is on angle while the long part is open in the middle, depth and tooling are fine and deflection is the variable. If the coupon is also off, you have an overall error rather than a distribution error. Look at program data, material or tooling instead of crowning.
Why more ram depth makes it worse
The intuitive correction fails, and this is where most setups go wrong. Added depth increases penetration by the same amount at the ends and in the middle, so the whole profile shifts down and the gap along the part stays. On the example above, a 2° error in the middle is roughly 0.1 mm of missing penetration. Dial that into the depth and the middle reaches 90° while the ends go to about 88°. The part is now wrong in two places instead of one.
When the crowning is set too high
Crowning works against deflection, so too much of it flips the pattern. The center closes and the ends stay put, or the ends flare open. The part looks wrong in the same place as a real canoe, which is why operators keep adding compensation to a problem that compensation created. It usually happens when a value calculated for a heavier or longer job, or left over from the previous run, is reused on a different thickness or V opening.
Set the crowning to zero and bend one part, then bend another at the programmed value. If the center moves from open to tight as the value increases, the setting is the problem, and this takes about thirty seconds to prove.
How to fix it
- Use the crowning system. Programmable crowning takes sheet thickness, length, die opening and tensile strength from the control and calculates the preload for each bend. Start from the calculated value, then fine-tune it from test bends. Our press brake crowning systems page explains how the mechanical and motorized options differ.
- Adjust in small steps. Change the value a little, bend a test piece and re-measure all five stations. Large changes overshoot into the opposite fault.
- Widen the V where the design allows. Stay within six to eight times thickness for mild steel. A wider opening lowers the force, and less force means less deflection. Do not go wider than the minimum flange allows.
- Check the machine is not overloaded. If a job runs close to full capacity over the full length, expect large deflection and little crowning margin.
- Without powered crowning, the fallback is shims or die adjustment. It is slow trial and error that produces scrap, so treat it as a stopgap for a fixed setup.
Cause 2: Tooling That Is Not One Straight Line
Crowning corrects the machine’s deflection curve and nothing else. No crowning system can compensate for poor punch and die alignment, and unevenly worn tooling forms parts with inconsistent angles, as the same crowning guide notes. This is the boundary that catches shops with a good crowning system and a persistent local error. Check these in the order they turn up:
- A joint under the part. Die blocks are butted together to make up the bed length. If the mating ends are not flush, or swarf sits under one block, the die surface has a step exactly where the error appears.
- Uneven shoulder wear. Most parts are bent through the middle of the machine, so the shoulder radius there wears first. The effective V geometry changes locally and the angle drifts in a center-weighted way that looks like deflection but does not respond to crowning the same way.
- Punch segments of different heights. Segments are ground as a set. A replacement from another set, or one not seated against its neighbor, sits proud and over-bends its section.
- Tool deflection. A tall gooseneck or a slender punch flexes under load too, and adds its own curve to the part.
The shift test separates all of these from the machine in one setup. Move the entire tooling package 200 mm to 300 mm along the bed, keep the same program and bend one part. If the defect moves with the tooling, it is the tooling. If it stays at the same spot on the bed, it is the machine or the material.
Fix: clean the tool seats, use one ground set of equal-height segments across the working length, and replace or regrind worn sections. Our tooling and tool storage solutions page covers options for organizing matched sets, and the tooling clamping system page covers holders that keep tools seated and aligned.
Cause 3: Material That Changes Along the Bend Line
A blank is not a constant, and the tolerance zone is wider than most shops assume. For 16-gauge sheet the permitted thickness range runs from 0.053 in to 0.067 in (1.35 mm to 1.70 mm), and A36 carries a tensile range from 55,000 psi to 79,800 psi against an average of 60,000 psi. The control cannot know which part of that range your blank came from, so it programs the average. Grain direction changes the forming pressure as well, as this review of angular variation adds.
Within one blank the spread is smaller, but it is not zero. Sheet is not perfectly parallel across the coil width, so if the blank is nested with the coil width running along the bend line, a thicker or stronger band under the middle of the part shows up as an angle that opens there.
How to confirm:
- Measure the bend angle at your five stations.
- Measure thickness with a micrometer at the same five stations, on the same side of the bend line.
- Lay the two profiles side by side. If the angle mirrors the thickness, the machine is behaving and the sheet is the variable. If the angle profile is smooth and symmetric while thickness is flat within about 0.01 mm, the machine is the variable.
Two related problems give the same complaint. A blank that is not straight, from camber in a sheared or slit strip, does not seat evenly on both die shoulders. A heavy burr on one edge holds that side off the die face. A straightedge and a feeler gauge show both.
Fix: cut blanks with the same grain direction, check incoming thickness, and keep batches together where accuracy matters. If the error follows the material, no machine adjustment removes it completely. Close the loop on each bend instead, with bending angle measurement that reads the angle during the stroke and corrects the depth.
Cause 4: Setup and Program Errors That Look Like Deflection
- Unequal ram position. If the ram reaches the bottom lower on one side, the part tapers from one end to the other. The signature is a straight slope, not a curve, and the end-for-end test confirms it. Have Y1/Y2 checked and calibrated.
- A table that is not flat in service. A long machine that has settled on its foundation, or sits on shims nobody revisited, can carry a twist along the bed. It shows as a taper that does not respond to Y1/Y2 correction and that changes when you move the load along the bed.
- Backgauge or sheet position. A backgauge that is not square, or a sheet that does not touch every finger, produces a taper that can read as a middle-of-part error on a short flange.
- Program data that does not match the setup. A part that is uniformly 3° off along its whole length is not a crowning problem, and no amount of compensation will make it one. Thickness, V opening, grade or springback allowance is entered wrong. Correct the program.
Calibration, level and alignment are cheaper to check on a schedule than to discover during a defect claim, which is what maintenance and upgrades is for.
Correcting It in the Right Order
Each step below either fixes the problem or removes a candidate. Done out of order, a setup turns into a morning of test bends.
- Profile two parts from the same setup at five stations, and note the orientation.
- Reseat the tooling. Clean the seats, check that blocks and segments are flush and from the same ground set, then run the shift test if the error is local.
- Mic the blank along the bend line and compare its thickness profile with the angle profile.
- Confirm the program data against the material actually loaded: measured thickness, real V opening, grade and the springback correction in use.
- Set crowning from a test bend, not from the display. Start from the calculated value, bend one part, measure the profile and step the value until the middle and the ends converge. Record it against material, thickness, length and tooling.
- If the crowning range runs out before the profile flattens, the machine’s structure is the limit at your tonnage. That is a specification problem, not a setting problem.
- If the tolerance is tight and the material keeps moving, close the loop on each bend with in-process angle measurement instead of correcting by hand at every setup.
Depth and crowning both change penetration, but only one of them changes how that penetration is distributed along the part. That is why the order matters.
| Correction | Changes penetration overall | Changes penetration along the length | What it is for |
|---|---|---|---|
| More ram depth (Y) | Yes | No | An angle that is uniformly off along the whole part |
| Crowning value | No | Yes, in a controlled curve | A symmetric canoe from deflection, or an inverse canoe from over-compensation |
| Shimming under the die | No | Yes, in steps | A last resort without powered crowning, for a fixed setup only |
| Reseating or replacing tooling | Partly | Yes, at the defect | A local step, a joint, a proud segment, uneven shoulder wear |
| Material control and sorting | Partly | Yes, wherever thickness varies | Blanks whose thickness profile maps onto the angle profile |
| In-process angle measurement | Yes, per part | Partly, as the loop corrects each bend | Material that varies between sheets, and tolerances too tight for setup-level correction |
If the tooling is right, the crowning is set from test bends, the material is consistent, and long parts still will not hold angle, the machine may be the limit. A press brake with no crowning, or with a short compensation range, will always struggle on long heavy bends. Where long parts with tight angular tolerance are the normal workload rather than the occasional job, the specification that decides whether the problem returns at every setup is the compensation system and the frame behind it, not the tonnage figure on the brochure. Models in the Genius CNC press brake series carry multi-point mechanical compensation with independently adjustable points along the table, which is the configuration long-part work with a real tolerance usually needs. For the rest of the line, start from the press brake range and match tonnage and bed length to your longest bend and heaviest material.
Five mistakes that recreate the problem
- Changing the program angle or ram depth to hide a middle error. It fixes the middle and breaks the ends.
- Adding crowning to a machine that has a tooling problem. The two errors cancel on one job and double on the next.
- Testing with a short strip and expecting the result to hold on a long part.
- Mixing tool segments of different heights or wear in one setup.
- Reusing one crowning value across different thicknesses and V openings.
If the angle is wrong in the same way on every part rather than varying along the length, crowning is not the subject. That is a springback or program data question, and it sits with the other bending defects in our press brake troubleshooting guide.
Send Us Your Bend Data
If the angle difference survives these checks, send us the following and our engineers will help you find the cause:
- Material type and grade, thickness and sheet length
- V opening and punch radius
- Target angle and the five measured angles, in order, with the orientation noted
- Machine model, bend length and tonnage used
- A photo or short video of the part and the setup
Reach the team through technical support with that data, and the first reply usually identifies which of the patterns above you are in.
This is one failure mode in a longer sequence. The press brake troubleshooting guide starts from the defect signature and narrows it to machine, tooling, material or method.
FAQ
Why is the middle of my part more open than the ends?
The ram and table deflect apart between the cylinders under load, so the punch penetrates less at mid-length than it does next to the uprights. Confirm it with a short coupon bent at mid-bed: if the coupon is on angle while long parts are open in the middle, deflection is the cause and crowning is the correction.
Is a 2° difference along a 3 m part normal?
It is common on long parts bent without deflection compensation, and it is the reason crowning exists. Whether it is acceptable is a question for your drawing and your customer. For diagnosis, what matters is whether the error repeats and where it sits on the part.
Can I fix it by increasing the ram depth or changing the program angle?
No. Depth moves the whole bend line, so the middle improves while the ends go under. The error is a difference in penetration along the length, and only something that changes the shape of the die line can remove it.
Why does a narrower V die make the variation worse?
It raises the tonnage needed per meter, which deflects the frame more, and it makes the angle more sensitive to small changes in material thickness and strength. For air bending mild steel we use six to eight times material thickness.
Does a short part have the same problem?
Shorter bends deflect less, but a short part bent in the middle of a long bed puts all the load in one place and can still show a difference. Bending it at another position, or using shorter tool segments, spreads the load differently.
What if the middle is too closed instead of too open?
That is over-compensation. The crowning value is larger than the deflection this job produces. Drop it toward zero, bend one part and work back up in small steps.