A fiber laser cutting machine is a CNC machine tool that cuts metal with a focused laser beam. The beam is generated inside a rare-earth-doped optical fiber, delivered to the cutting head through a flexible cable, and concentrated onto the workpiece, where it melts the metal while a coaxial jet of assist gas blows the molten material out of the kerf. Nothing touches the sheet — no blade, no die, no cutting force.
What matters if you are evaluating one:
- “Fiber” describes where the beam is made and how it travels, not what it cuts. Every machine in this class cuts metal. None cut acrylic, wood or glass.
- The source sets the ceiling on thickness. The head, gas supply and motion system decide whether you reach that ceiling every shift.
- Maximum thickness and economic thickness are different numbers, and only one appears in a brochure.
- On stainless and aluminum, assist gas is frequently the largest line in the hourly running cost — larger than electricity.
- Cut quality is a specification, not an opinion. An ISO standard defines it, and most purchase orders never mention it.
How Does a Fiber Laser Cutting Machine Work?

Six stages, in the order they happen.
1. Generation. Pump diodes excite the doped fiber; stimulated emission produces a coherent beam at roughly 1.07 µm. Output power and beam quality (beam parameter product, or BPP) are set here, and they are not the same thing — a tighter beam focuses to a smaller, brighter spot and holds a narrower kerf.
2. Delivery. The beam travels to the cutting head through a fiber cable and a connector. A contaminated connector face absorbs energy; absorbed energy becomes heat; heat destroys connectors. This is a handling issue, not a laser fault, and it is one of the most common causes of a machine that “suddenly lost power”.
3. Focusing. A collimator straightens the beam and a focusing lens concentrates it onto the sheet. In front of the lens sits a protective window — a cover slide that takes the spatter so the lens does not have to. It is a consumable, and on thick plate with heavy piercing it is a consumable with a short life.
4. Melting. The metal absorbs energy and melts at the focal point. Too little power and the cut fails to penetrate; too much heat input and you get a wider heat-affected zone, heavy dross and dimensional drift. Focus position is a per-material setting, not a machine setting.
5. Gas removal. A coaxial jet through the nozzle ejects the molten metal and shields the optics from spatter and fume. Gas also sets the chemistry of the cut face, and chemistry is where money and quality collide.
6. Motion. The CNC turns a CAD file into path, pierce points, sequence and parameters, then drives the servo axes. Standoff is held by capacitive sensing, because the process is unforgiving: a fraction of a millimeter of height error turns a clean cut into a drossy one. On thin sheet with dense nesting the machine spends its time accelerating and turning, so acceleration and corner behavior predict cycle time far better than a top-speed figure.
Which assist gas should you use?
| Material | Gas | Edge | Downstream | Cost driver |
|---|---|---|---|---|
| Mild steel, thick | Oxygen | Oxide layer, wider kerf | Must be cleaned before paint or weld | Low pressure, low volume |
| Mild steel, thin, to be coated | Nitrogen or air | Clean, paint-ready | Skips a cleaning step | High volume |
| Stainless | High-pressure nitrogen | Bright, oxide-free | Ready to weld or finish | Gas can dominate hourly cost |
| Aluminum | Nitrogen | Dross control is the variable | Alloy and surface matter as much as settings | High volume |
| Galvanized | Air or nitrogen | Acceptable edge, zinc fume | Extraction and filter life | Filtration, not gas |
| Copper, brass | Nitrogen, source rated for reflection | Good, with tight pierce control | Back-reflection is the limiting factor | Source specification |
The relationship inverts with thickness, and that is the part buyers miss. Oxygen is reactive: it burns the steel and adds energy, so you need very little of it, and a modest-power machine can still get through thick mild steel. Nitrogen is inert: it only blasts the melt out, which takes high pressure and a large volume of gas. The thicker the work, the less oxygen you need and the more nitrogen you need. On a stainless-heavy part mix, the gas contract can decide whether the job makes money — and it is often quoted separately, sometimes not at all.
What Are the Main Components?
| Component | Function | Why it matters |
|---|---|---|
| Fiber laser source | Generates the beam | Sets power and beam quality |
| Cutting head | Focuses the beam onto the sheet | Precision and stability |
| CNC controller | Controls paths and parameters | Accuracy and repeatability |
| Servo motors and drives | Move the axes | Positioning and dynamic response |
| Bed and gantry | Carry the structure and motion | Rigidity under acceleration |
| Assist gas system | Removes molten material | Edge quality, speed, running cost |
| Water chiller | Cools source and optics | Stable operating temperature |
| Extraction system | Removes fume and particles | Air quality and operator safety |
A high-power source cannot compensate for a flexible gantry, a tired nozzle or an undersized gas supply. Evaluate the machine, not the wattage.
Why Two 6 kW Machines Do Not Cut the Same Part the Same Way
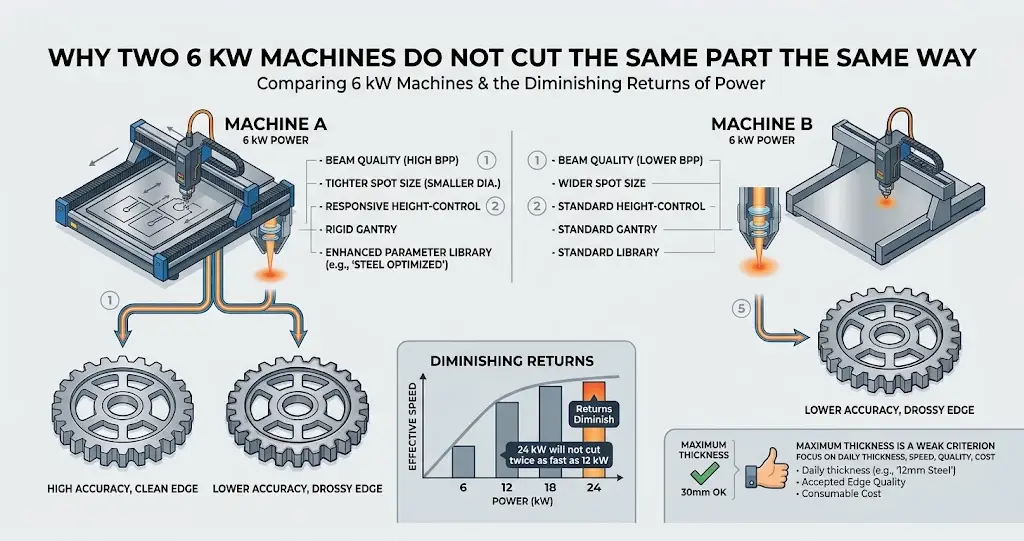
“6 kW, 3015, exchange table” describes a class of machine, not a capability. Beam quality, spot size at focus, the height-control loop, how well the parameter library was developed for your materials, gas delivery capacity and gantry rigidity all move the result.
Power also stops paying as it climbs. As The FABRICATOR reported in a 2025 review of large-format plate cutting, “24 kW of power will not cut twice as fast as 12 kW” — returns diminish, especially in thicker material.
Which is why “maximum cutting thickness” is a weak selection criterion on its own. Every supplier can demonstrate a pierce at the extreme of the range. The number that matters is the thickness you cut every day, at a speed and edge quality your customer accepts, with a consumable cost you can live with.
When the Cut Goes Wrong, Which Part Owns It?
| What you see | Usual owner | Check first |
|---|---|---|
| Dross under mild steel, worse on one side of the part | Nozzle or beam alignment | Is the beam centered in the nozzle? |
| Heavy dross on stainless with a rounded top edge | Focus position or gas pressure | Focus height, then pressure and purity |
| Cuts drop out at random places mid-sheet | Height control or material | Slat wear, sheet flatness, protective window |
| Wide kerf and heavy tint on thin sheet | Power, speed or focus | Too much power or too slow a feed |
| Piercing thick plate shatters the protective window | Pierce parameters | Pierce height, pierce time, ramp-in |
| Edge takes powder coat badly | Gas choice | Oxygen leaves an oxide the coater rejects |
The pattern is consistent: the laser source is the least likely suspect and the most expensive thing to replace. Diagnose the chain from the nozzle backwards.
Cut Quality Is a Number, Not an Opinion

Buyer and supplier both say “good cut quality”, neither defines it, and the argument starts on the day the first batch is inspected. There is an international answer: ISO 9013 sets out geometrical product specifications and quality tolerances for classifying thermal cuts, and it explicitly covers laser cuts from 0.5 mm to 32 mm. It only applies when the drawing or delivery condition references it — which is exactly why you should reference it.
Before the machine ships, agree in writing: the acceptance coupon (material grade, thickness, gas, nozzle, program); what gets measured (dimensions, perpendicularity, dross and burr, hole roundness, cycle time); who measures and with what; and the thickest and thinnest jobs in your mix, not just the comfortable middle. A supplier who resists this is telling you something useful.
Safety, in Three Documents
IEC 60825-1 classifies laser products. A properly enclosed machine with intact interlocks and correctly specified viewing windows is Class 1 in operation — the beam is inaccessible, which is what allows operators to work beside it without laser eyewear. That classification depends on the interlocks working.
ISO 11553-1:2020 adds the machine-specific layer, including the information a manufacturer must supply beyond IEC 60825. The safety documentation package is a legitimate line on your comparison sheet, not paperwork to wave through.
OSHA’s Technical Manual covers classification, the Laser Safety Officer role, engineering controls and laser-generated air contaminants: local exhaust ventilation at the kerf is the primary control. A machine without adequate extraction has a fume problem, whatever the enclosure looks like.How to Specify One Without Overbuying
- Part mix, by hours rather than part count. Materials, thicknesses, and the share of machine time each represents.
- Sheet format and how sheets reach the table. 3015 is the economical default; 4020 and 6020 earn their footprint only if the work is genuinely large-format.
- Table type. A single table suits low-mix work. An exchange table pays wherever loading is a real fraction of the cycle.
- Power, against economic thickness. If most of your hours sit under 3 mm, a 12 kW machine is a throughput argument, and it needs a cycle-time calculation to support it.
- Gas supply. Bulk tank, generator or cylinders — plus the space and contract each one needs.
- Extraction, power, foundation. Boring, and the usual reason an install slips two weeks.
- Acceptance protocol and first spares order. Nozzles, protective windows and lenses should arrive with the machine, not three weeks after the first production run.
Where CAMT Fits
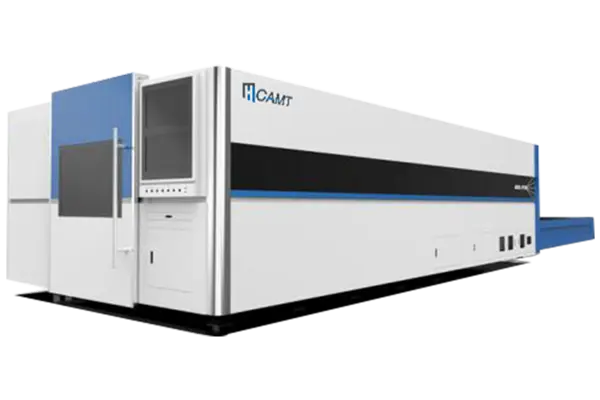
We build fiber laser machines for shops that need the machine to work, not to be a showcase. An open-type single-table cutter suits small and medium workshops that want a compact footprint. An enclosed exchange-table machine suits production work where loading time is the bottleneck and the enclosure matters for both safety and fume control. A tube and pipe laser handles round, square and rectangular profiles with 3D bevel capability. The full range and specification table sit on the laser cutting machine page. If you are still fixing the specification, how to choose a fiber laser cutting machine walks through the same decision step by step.
Two things we do that are worth more than a datasheet: we tell you when a configuration is wrong for your part mix — including when plasma or oxyfuel suits your thickness better — and we treat nozzles, protective windows and lenses as the consumables they are, backed by technical support rather than a spare-parts catalogue and a hope.
Most of our customers cut and then bend, so the press brake range is worth reviewing at the same time: the edge your laser leaves is the edge your brake forms. Send your material and thickness list, sheet sizes and monthly hours through our contact page and we will come back with a configuration and the reasoning behind it — including the reasoning that argues against the bigger machine.
FAQs: What Is a Fiber Laser Cutting Machine and How Does It Work?
What thickness can a fiber laser cut?
It depends on power, gas, material grade and the edge quality you accept, which is why a single maximum figure is close to meaningless. Ask for two numbers: what the machine can pierce and cut, and what it cuts economically. Then cut a sample in your material and measure it.
Is fiber better than CO2?
For metal, almost always: higher absorption at the shorter wavelength, faster on thin gauge, no laser gas, no mirror path. For non-metals it is the wrong tool. Mixed metal and non-metal shops usually keep a separate CO2 machine. For the full cost, speed and application comparison behind that answer, see our fiber laser vs CO2 laser comparison guide.
Can it cut copper and brass?
Yes, with conditions. Both reflect part of the beam back toward the head, so pierce control has to be tighter and the source should be rated for reflective work with optical isolation. Get in writing whether the configuration is rated for continuous reflective work or occasional jobs, and what the warranty position is if back-reflection occurs.
What does it cost to run?
Electricity, assist gas, consumables and spares. Electricity is usually the smallest. Gas is often the largest on stainless and aluminum, and almost negligible on thick mild steel cut with oxygen. Consumables mean nozzles, protective windows and eventually lenses, and they scale with how much thick-plate piercing you do.
Open machine or enclosed machine?
The enclosure is not only a safety upgrade. On an exchange-table model it is what lets you cut continuously, contains sparks and fume, and keeps the cutting zone stable. The open machine is cheaper, easier to load by hand, and adequate for low volume and prototype work.
Do I need a special building?
Check three things before the machine lands: power capacity and stability at the nameplate rating, including the chiller; a gas arrangement sized for real consumption; and extraction ducted somewhere legal. Add floor loading and the access route — an exchange-table frame does not move with a pallet truck afterwards.